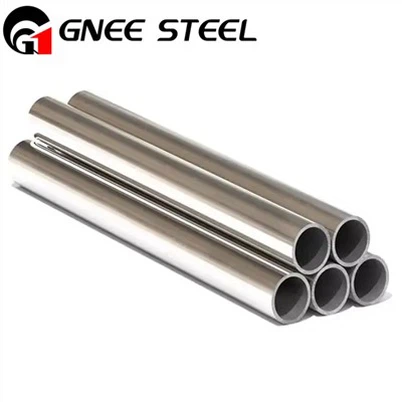


ASTM A213 TP316L stainless tube heat exchanger
Leave a message
If you are seeking highly reliable ASTM A213 TP316L stainless steel tubes for heat exchangers, we offer tubing that complies with standards such as ASTM A213 / ASME SA213, EN 10216-5, and GB/T 13296, designed to meet the demands of rigorous operating conditions and long-term service.
What are the advantages of ASTM A213 TP316L heat exchanger tubes?
TP316L features a low-carbon composition (C ≤ 0.03%), which effectively prevents intergranular corrosion following welding. Additionally, containing 16–18% Cr, 10–14% Ni, and 2–3% Mo, it demonstrates superior resistance to pitting and general corrosion in acidic and chloride-containing environments.
GNEE supplies high-quality SS 316L steel tubes specifically designed for heat exchangers. These tubes are manufactured using processes such as vacuum refining, solution annealing (1040–1100°C), and pickling and passivation, ensuring a uniform microstructure and a clean surface finish. We offer both seamless and welded heat exchanger tubes, with outer diameters ranging from 6 mm to 273 mm and wall thicknesses ranging from 0.8 mm to 25 mm.
Our product range includes straight tubes, U-tubes, and coiled tubes; the internal surface roughness is controlled to Ra ≤ 0.8 μm, and the tube ends are cut squarely and deburred. These features effectively enhance heat exchange efficiency. Suitable for operating temperatures ranging from approximately -196°C to 550°C, these steel tubes are widely utilized in the petrochemical industry, pharmaceutical equipment, food processing, and various heat exchange systems.


In addition, we also supply heat exchanger tube sheets.
Click to Customize TP316L Heat Exchanger Tubes
ASTM A213 TP316L Dimensions & Surface Quality
| Feature | Requirement / Specification | Reference Standard |
| Material Grade | TP316L (UNS S31603) - Low Carbon | ASTM A213 |
| Manufacturing | Seamless (SMLS), Cold Finished | ASTM A213 |
| Condition | Solution Annealed & Pickled (AP) or Bright Annealed (BA) | ASTM A213 |
ASTM A213 stianlesssteel pipe Dimensional Tolerances
Note: Heat exchanger tubes are typically ordered to Minimum Wall (MW) thickness.
| Parameter | OD Size Range | Tolerance |
| Outside Diameter (OD) | ≤ 1.000" (25.4 mm) | ± 0.004" (0.10 mm) |
| > 1.000" to 1.500" excl. | ± 0.006" (0.15 mm) | |
| 1.500" to 2.000" excl. | ± 0.008" (0.20 mm) | |
| Wall Thickness (WT) | All Sizes | + 20% / - 0% (for Minimum Wall) |
| Optional (Average Wall) | ± 10% (must be specified in PO) | |
| Length | ≤ 24 ft (7.3 m) | + 1/8" (3 mm) / - 0" |
| > 24 ft (7.3 m) | + 1/8" per 10ft / - 0" (max +1/2") | |
| Ovality (Out-of-round) | All Sizes | Included in OD tolerance |
| Straightness | All Sizes | Max 0.030" per 3 ft (or 1 mm / 1 m) |
ASTM A213 UNS S316l00 Seamless Tubes Chemical Composition
| Grade | Carbon | Manganese | Silicon | Phosphorus | Sulfur | Chromium | Molybdenum | Nickel | |
| 316L | Minimum | 16.0 | 2.0-3.0 | 10.0 | |||||
| Maximum | 0.035 | 2.0 | 0.75 | 0.045 | 0.030 | 18.0 | 14.0 | ||
Physical Properties of SA213 TP316L Seamless Tube
| Grade | Specific Heat 0-1000C (J/kg.K) | Density (kg/m3) | Elastic Modulus (GPa) | Thermal Conductivity (W/m.K) | Mean Coefficient of Thermal Expansion (m/m/0C) | Electrical Resistivity (n.m) | |||
| at 1000C | at 5000C | 0-1000C | 0-3150C | 0-5380C | |||||
| 316L | 500 | 8000 | 193 | 16.3 | 21.5 | 15.9 | 16.2 | 17.5 | 740 |
Mechanical Properties of ASTM A213 SS 316L Tube
| Material | Heat | Temperure | Tensile Strength | Yield Strength | Elongation %, Min |
| Treatment | Min. º F(º C) | Ksi (MPa), Min. | Ksi (MPa), Min. | ||
| TP316L | Solution | 1900 (1040) | 70(485) | 25(170) | 35 |
Surface Quality & Finish
| Feature | Specification Requirement |
| Internal Surface | Scale-free, smooth, and free from longitudinal defects. |
| External Surface | No cracks, laps, seams, or deep scratches. |
| Surface Roughness | Ra ≤ 0.8 μm (32 μin) for ID/OD |
| Cleanliness | Free from oil, grease, drawing lubricants, and metal particles. |
| Passivation | Chemical passivation required after pickling. |
| Ends | Plain ends, square cut, de-burred (no sharp edges). |
Heat Treatment (Solution Annealing)
Temperature: Minimum 1900°F (1040°C).
Quenching: Rapid cooling in water or air to prevent chromium carbide precipitation (Sensitization).
Certification: MTC must state the actual heat treatment temperature and cooling method.
What points should be considered when purchasing ASTM A213 TP316L stainless steel tubes?
Minimum Wall vs. Average Wall:
Always specify "Minimum Wall" for heat exchangers to ensure the tube meets the design pressure calculations at its thinnest point. ASTM A213 defaults to Minimum Wall unless otherwise stated.
U-Bend Tubes (if applicable):
If ordering U-tubes, specify Stress Relieving for the bend area and Wall Thinning Allowance (typically the back of the bend thins by ~10%).
Specific Ra Requirements:
If your process involves high-purity media or heavy fouling, specify a lower Ra (e.g., Ra < 0.5 μm).
Tube-to-Tubesheet Expansion:
Specify a Maximum Hardness (e.g., 80-85 HRB). If the tube is too hard, it will not expand properly into the tubesheet, leading to bypass leaks.
TP316L Stainless Steel Tube Heat Exchanger Manufacturer
Reference Monthly Capacity: The typical monthly output for TP316L ranges from 500 to 800 tons.
Specification Coverage: Common specifications for heat exchanger tubing typically range from OD 15.88 mm to 38.1 mm.
Production Lead Time
Stock/Modification: 3–7 days (involves cutting, cleaning, and packaging only).
Standard Production: 35–50 days.
Rush Orders: 21–28 days.
Influencing Factors: If U-bending processing is required, the lead time will be extended by an additional 7–10 days.


Supplementary Testing
|
- Eddy Current Testing - O.P Testing - Radiography Testing |
- Corrosion Testing - Micro Testing - Macro Testing |
- IGC Testing - Ultrasonic testing - Liquid Penetrate testing |


Professional Packaging
ASTM A213 TP316L heat exchanger tubes feature thin walls (typically 1.5 mm to 2.5 mm); therefore, packaging must be designed to prevent bending, deformation, and surface scratches.
End Caps: Both ends of every tube must be fitted with protective caps to prevent dust ingress or moisture accumulation within the interior walls.
Export-Grade Fumigated Plywood Cases: The tubes are stacked in layers within the wooden crates, with each layer separated by wooden boards or soft cushioning materials.
Special Considerations:
Marking: The exterior of the crate must be clearly marked with the following information: Standard (ASTM A213 TP316L), Size (OD x WT x L), Heat No., Weight, as well as warning symbols such as "Do Not Stack" and "Keep Dry."